Key Takeaways & Executive Findings
- •• • At 1200 °C thermal cycling, BPS coatings survive 250 cycles without spallation, whereas 8YSZ fails at 150 cycles—a ≥67% lifetime extension. This directly reduces unplanned turbine shutdowns and maintenance intervals, critical for power generation and aviation fleets. • • Vacuum heat treatment after 400 h isothermal oxidation reduces oxide content by ~80% and porosity by ~90%, effectively healing defects and suppressing bond-coat degradation. This post-processing step can extend coating service life by mitigating TGO growth and interfacial stress concentration. • • CMAS and molten-salt corrosion remain primary failure accelerators; Al2O3–TiO2 codoping and Sc2O3–Y2O3 co-stabilization improve resistance, but quantitative corrosion rates under combined CMAS/water-oxygen environments are lacking, necessitating standardized testing protocols. • • Multi-component and high-entropy rare-earth zirconates exhibit low thermal conductivity and enhanced phase stability, yet long-term cycling data beyond 500 h are scarce. Industrial adoption requires validated performance metrics and cost parity with conventional YSZ.
China Advanced Materials & Deep-Tech Radar
Get verified English translations, SEM micrographs & open-access PDF alerts from China's leading state key laboratories delivered to your inbox every Monday at 08:00 EST.
Abstract
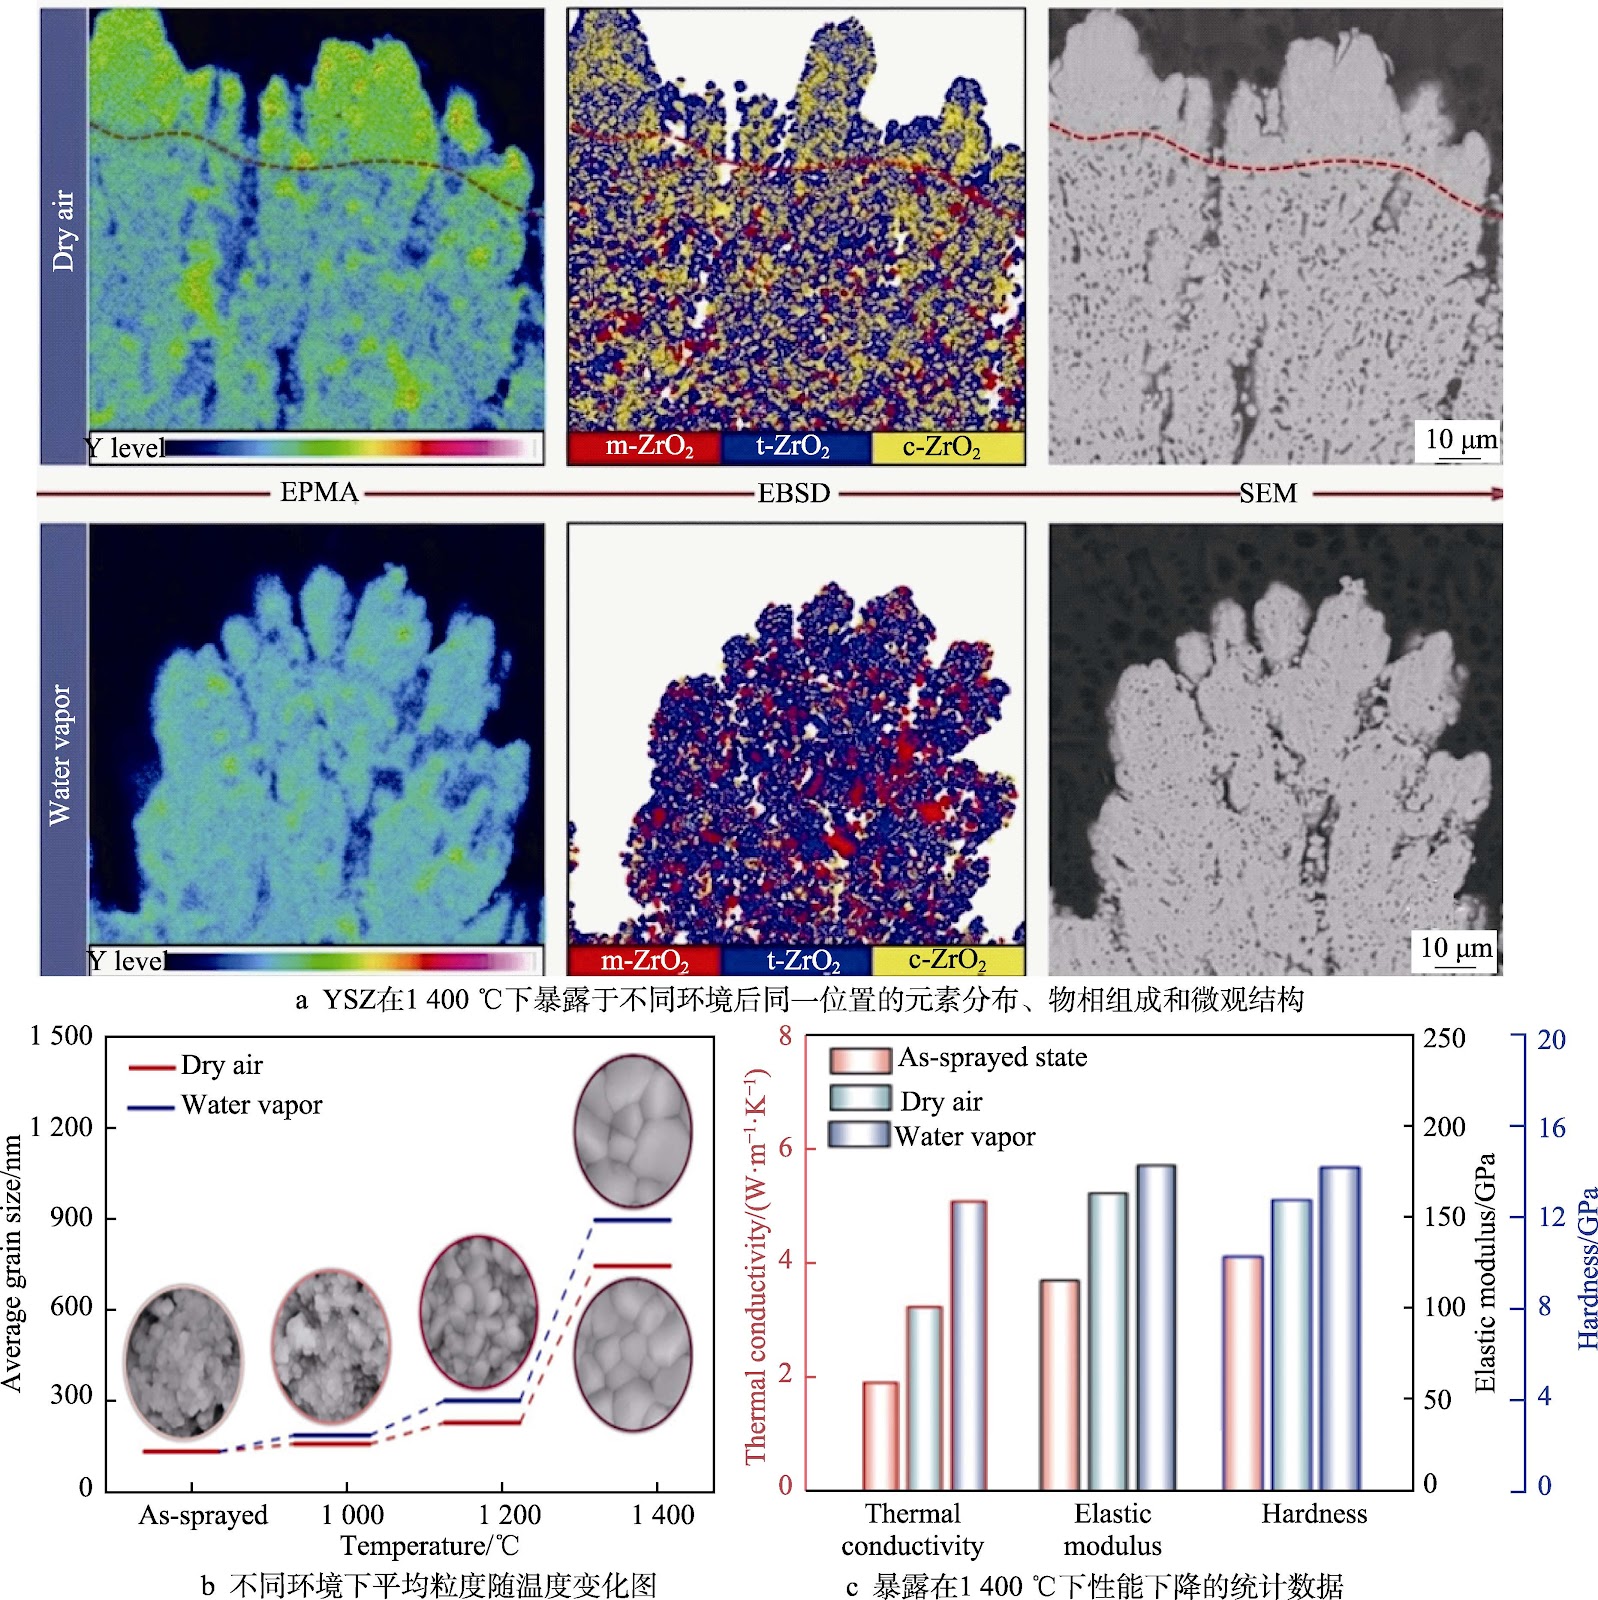
Thermal barrier coatings (TBCs) are critical for protecting aero-engine and gas-turbine hot-section components, yet conventional yttria-stabilized zirconia (YSZ) coatings degrade severely above 1200 °C through phase destabilization, sintering-induced densification, and environmental attack. This review systematically analyzes high-temperature failure mechanisms governed by coupled oxidation, residual stress, and corrosion. Key degradation modes include thermally grown oxide (TGO) thickening and interfacial rumpling, tetragonal-to-monoclinic phase transformation in YSZ, CMAS and molten-salt infiltration, and water-oxygen synergistic erosion. The dynamic interrelations and nonlinear characteristics of these failure modes are clarified. Efficiency enhancement strategies are categorized into compositional optimization (novel ceramics, multi-component solid solutions, reactive-element doping), microstructural design (lamellar, columnar, and functionally graded architectures), and post-treatment (laser remelting, vacuum heat treatment). Quantitative benchmarks demonstrate that at 1200 °C thermal cycling, BPS coatings remain intact after 250 cycles versus spallation of 8YSZ at 150 cycles, indicating a ≥67% lifetime improvement. Vacuum heat treatment suppresses bond-coat damage, reducing oxide content by ~80% and porosity by ~90% after 400 h isothermal oxidation. These findings provide a theoretical and technical basis for rational design of next-generation high-performance, long-life TBCs.
1. Introduction
Conventional yttria-stabilized zirconia (YSZ) thermal barrier coatings have reached a performance ceiling. Above 1200 °C, the tetragonal phase transforms to monoclinic, accompanied by ~4% volume expansion that initiates microcracks; sintering densifies the porous structure, raising thermal conductivity and reducing strain tolerance; and CMAS infiltration dissolves the stabilizer, triggering catastrophic spallation. These coupled degradation modes cause premature failure, with 8YSZ coatings spalling after only 150 cycles at 1200 °C, far short of next-generation turbine requirements.
This review addresses the bottleneck by systematically dissecting failure mechanisms and evaluating enhancement strategies. It quantifies the interplay between TGO thickening, residual stress, and corrosion, and benchmarks advanced architectures and compositions. Notably, BPS coatings achieve 250 cycles under identical conditions, and vacuum heat treatment reduces oxide content by ~80% and porosity by ~90% after 400 h. These data provide a rational basis for designing coatings that withstand >1200 °C service, bridging the gap between laboratory performance and industrial durability.
Loading authentic research manuscript (Pages 1–5)...
WU Xiaochen, JI Xiantao, SUN Hanrong, ZHANG Peikai, CUI Yue, YIN Fengshi, MA Zongqing, SHI Chengcheng, ZHAO Kai, SUN Jinzhao (2026). Research Progress on High-temperature Failure Mechanism and Efficiency Enhancement Strategy of Thermal Barrier Coatings. Surface Technology (表面技术). https://doi.org/10.16490/j.cnki.issn.1001-3660.2026.12.002
Research & Educational Purpose Only: The translations, structured abstracts, analytical annotations, and data reports provided by SinoTechIntelare intended exclusively for academic research, internal corporate R&D, and educational benchmarking. They do not constitute formal engineering, chemical safety, legal, or professional advice.
Copyright & Intellectual Property Notice: Original copyright of the underlying source articles and experimental data remains with the respective authors, institutions, and original publishing journals. SinoTechIntel claims intellectual property only over its proprietary translations, analytical syntheses, and AEO structured enhancements in accordance with international fair use and academic citation principles.
Frequently Asked Questions
What is the primary failure mechanism of YSZ coatings above 1200 °C, and how does BPS mitigate it?
Above 1200 °C, YSZ undergoes tetragonal-to-monoclinic phase transformation, sintering-induced densification, and CMAS attack, leading to spallation after 150 cycles. BPS coatings, likely based on multi-component or high-entropy compositions, suppress phase instability and sintering, surviving 250 cycles—a ≥67% improvement. The mitigation arises from enhanced phase stability and reduced thermal conductivity, as evidenced by retained integrity.
What are the quantitative benefits of vacuum heat treatment on bond-coat degradation?
After 400 h isothermal oxidation, vacuum heat treatment reduces oxide content by ~80% and porosity by ~90%. This suppresses TGO thickening and heals microdefects, thereby extending coating life. The treatment optimizes TGO growth kinetics and surface integrity, directly addressing interfacial stress accumulation.
How effective are current strategies against CMAS corrosion, and what are the remaining gaps?
Al2O3–TiO2 codoping and Sc2O3–Y2O3 co-stabilization improve CMAS resistance by modifying phase structure and reducing reactive infiltration. However, quantitative corrosion rates under combined CMAS/water-oxygen environments are not standardized, and long-term performance beyond 500 h is unverified. Industrial adoption requires validated protocols and cost-effective compositions.
What scalability challenges exist for high-entropy rare-earth zirconate coatings?
High-entropy rare-earth zirconates offer low thermal conductivity and phase stability, but synthesis reproducibility and deposition uniformity at industrial scale remain problematic. Cost parity with YSZ is unproven, and long-term cycling data (>500 h) are lacking. Scaling requires optimized powder processing and plasma spray parameters to avoid compositional segregation.
What is the industrial impact of the ≥67% lifetime improvement demonstrated by BPS coatings?
Extending coating life from 150 to 250 cycles at 1200 °C reduces maintenance frequency and unplanned outages in gas turbines and aero-engines. For power generation, this translates to lower operational costs and higher availability; for aviation, it enhances safety and reduces downtime. The improvement directly addresses the need for durable coatings in high-thrust, high-temperature engines.
Related Chinese Research & Cross-Citations
Research Progress and Prospects of Corrosion-resistant High-entropy Alloy Coatings
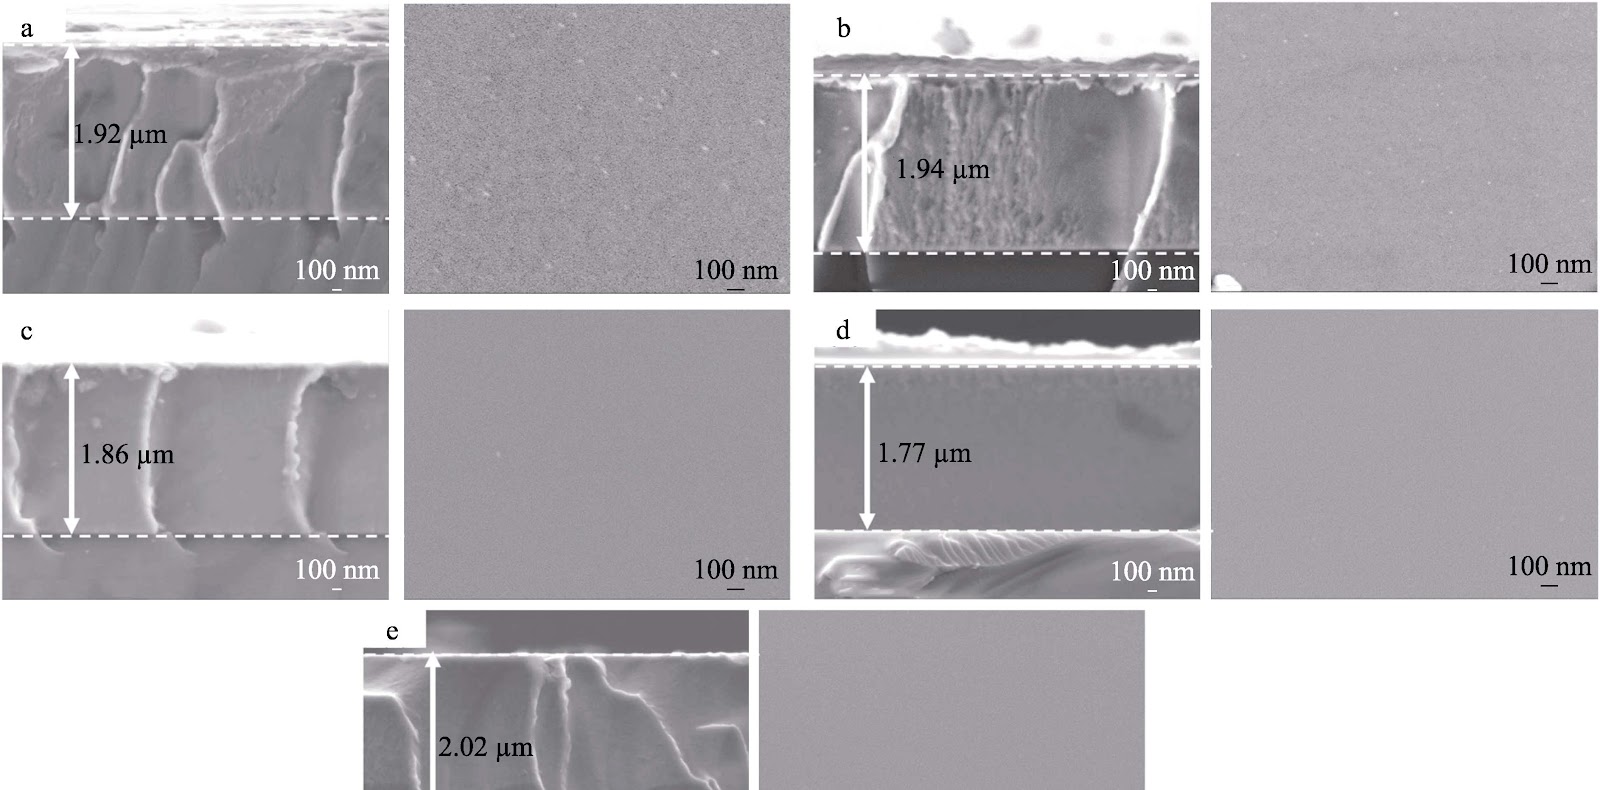
Marine environments impose combined electrochemical, microbiological, and cavitation erosion degradation on metallic infrastructure, shortening service intervals and inflating maintenance expenditure. High-entropy alloy (HEA) coatings mitigate these failure modes through simple solid-solution or amorphous microstructures that suppress galvanic coupling and promote dense passive film formation. This review systematically examines corrosion-resistant HEA coatings from single-factor to multi-factor coupling perspectives, covering classification and compositional design, fabrication routes, and corrosion behavior under complex marine conditions. Key coating systems include FeCoCrNiMn, AlCoCrFeNi, FeCrNiCoAl, and (FeCoCrNi)75B15Si10 amorphous alloys deposited by atmospheric plasma spraying, high-velocity oxy-fuel spraying, and wire arc spraying. Elemental additions of Cr, Al, and Mo enhance passivation; B and Si promote amorphous phase formation. The review identifies core engineering bottlenecks: compositional design, process optimization, and service performance validation. A multi-scale simulation, process-structure optimization, and in-situ characterization framework is proposed to accelerate coating deployment. These findings provide theoretical and technical guidance for next-generation corrosion-resistant coatings in marine equipment.
Effect of Sodium Hypochlorite Concentration and Medium Temperature on Corrosion of 45# Steel in Artificial Seawater and Simulated Concrete Pore Solution
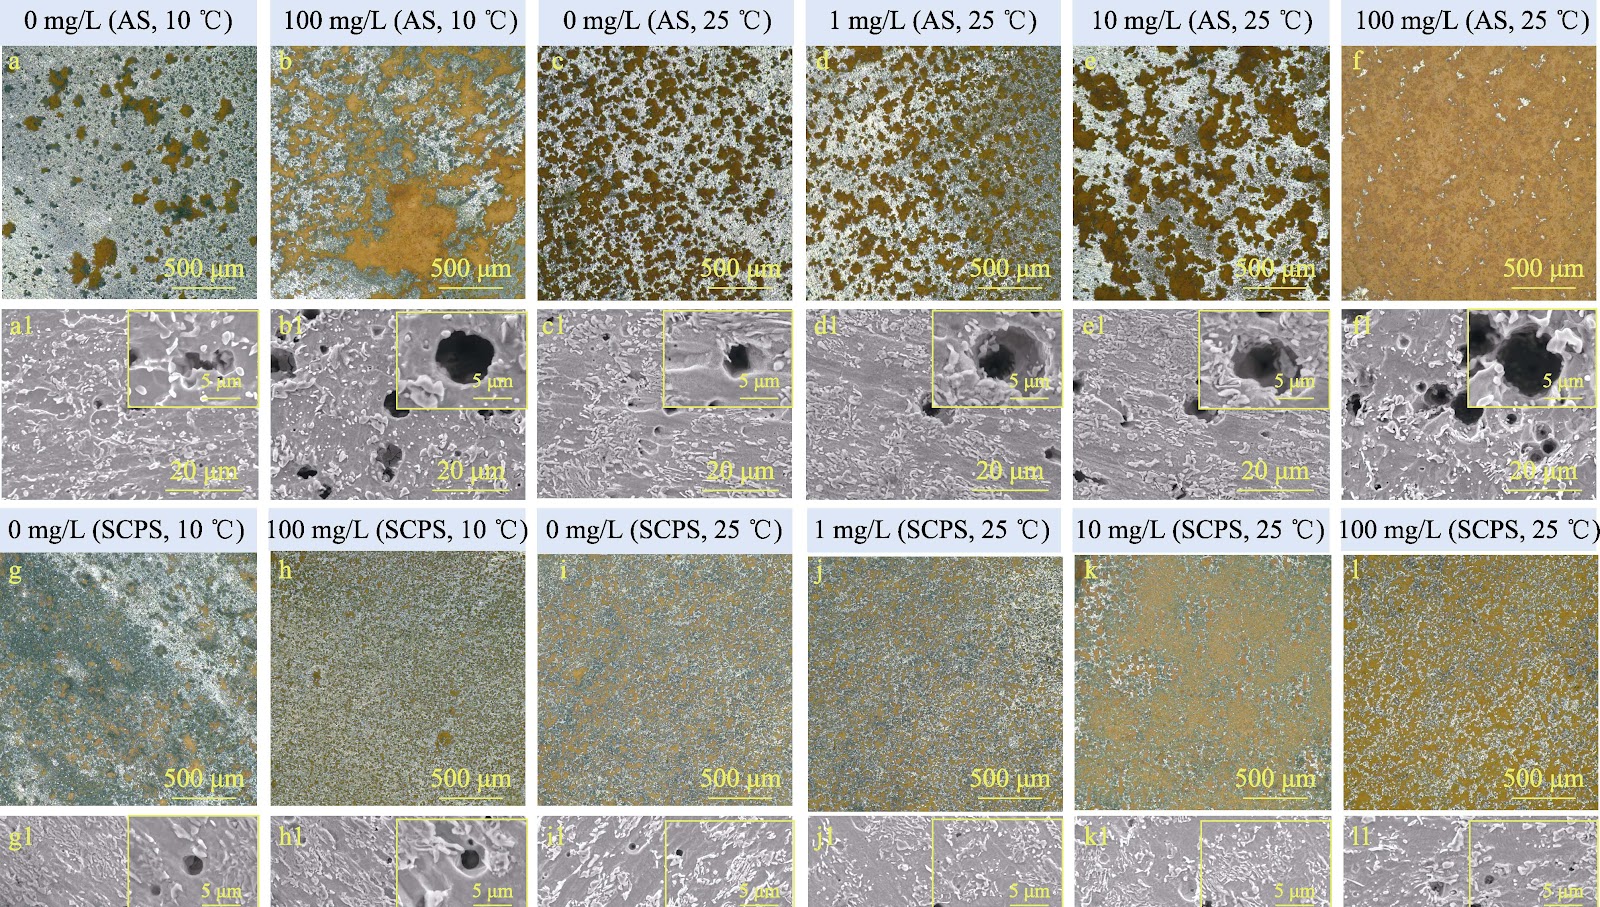
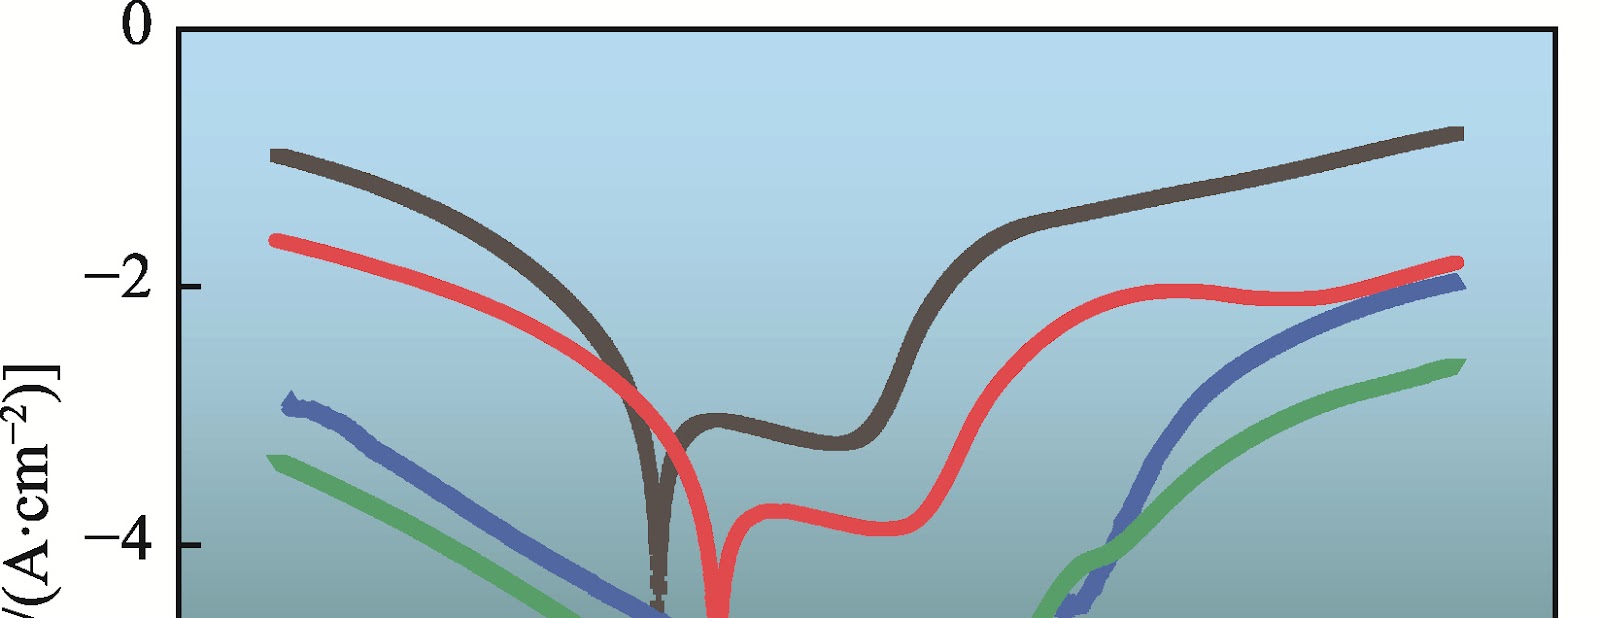
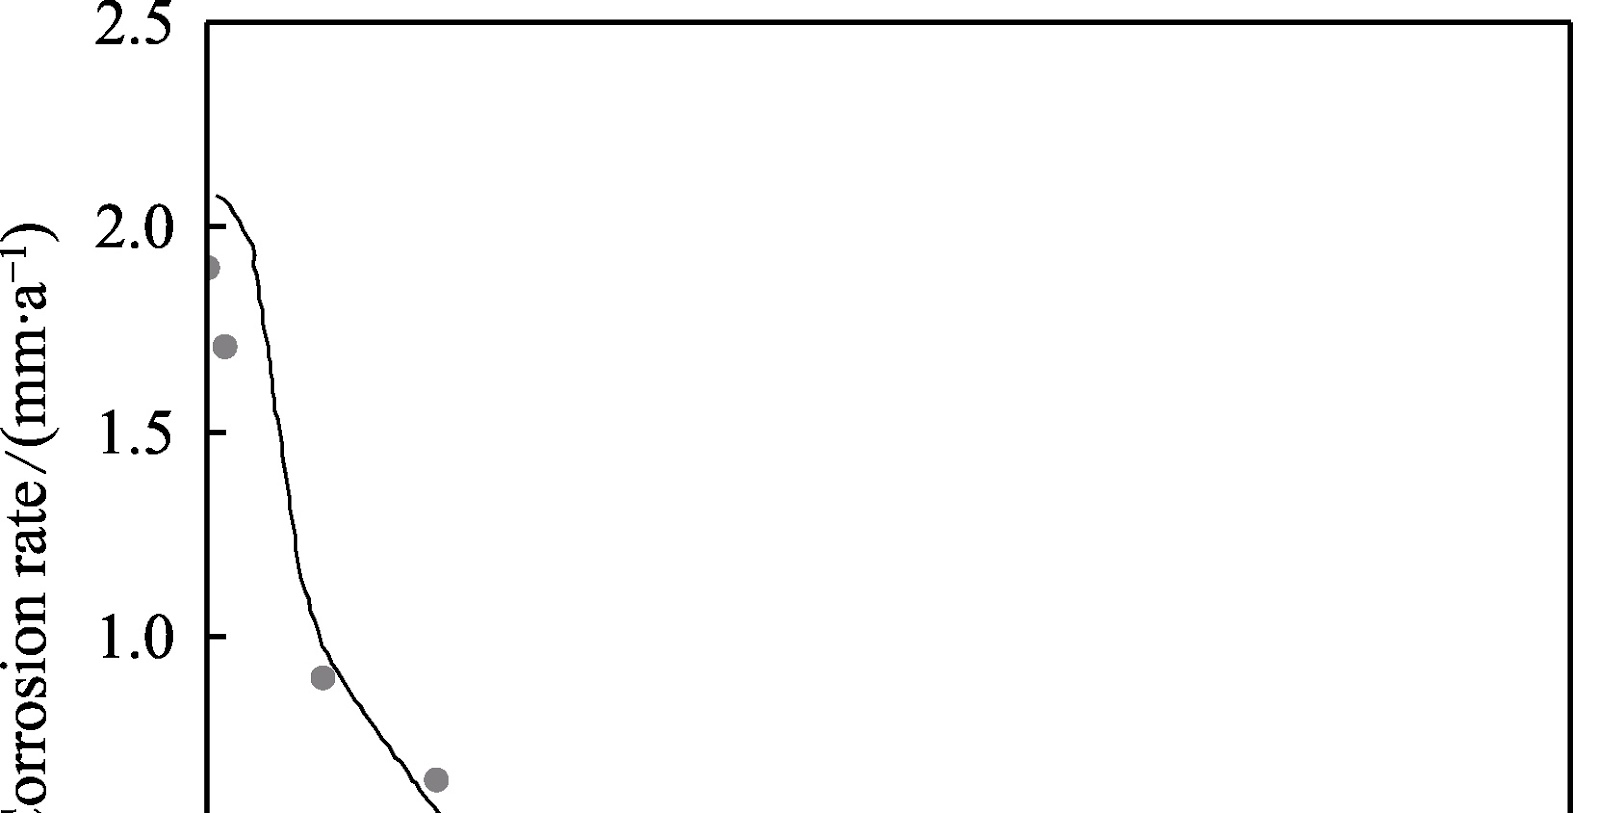
Seawater discharged during LNG regasification carries residual chlorine, predominantly sodium hypochlorite (NaClO), and low temperature, posing a dual corrosion threat to carbon steel components and adjacent reinforced concrete. This study systematically evaluates the corrosion behavior of 45# steel in artificial seawater (AS) and simulated concrete pore solution (SCPS, pH≈10) under NaClO concentrations of 0, 1, 10, and 100 mg/L at 10 °C and 25 °C. Electrochemical impedance spectroscopy, potentiodynamic polarization, weight-loss measurements, and localized corrosion-depth analysis were combined with SEM, EDS, XPS, and XRD to resolve corrosion kinetics, morphology, and product composition. In AS at 25 °C, increasing NaClO from 0 to 100 mg/L decreased charge transfer and film resistance (Rct + Rf) from 2266 to 1207 Ω·cm² and increased corrosion current density (Jcorr) from 11.48 to 18.29 μA/cm². Weight-loss rates remained 0.108 mm/a at 0 and 1 mg/L NaClO, rose slightly to 0.123 mm/a at 10 mg/L (+13%), and sharply to 0.202 mm/a at 100 mg/L (+87%). Corrosion morphology shifted from localized to uniform, with reduced pit depth. In SCPS at 25 °C, the alkaline environment suppressed NaClO-induced acceleration: Rct + Rf decreased from 2922 to 2266 Ω·cm², and weight-loss rates increased only 8% (0.0937 mm/a) at 10 mg/L and 25% (0.108 mm/a) at 100 mg/L relative to the 0.0865 mm/a control. However, 100 mg/L NaClO in SCPS significantly deepened localized pits. At 10 °C, both media exhibited reduced corrosion current density, thinner product layers, and shallower pits. Under standard discharge conditions (residual chlorine ≤0.2 mg/L), the additional corrosion risk from cold discharge water is negligible.
Corrosion Inhibition Mechanism of Typical Inorganic Inhibitors on Stainless Steel in a Simulated Electrolytic Seawater Environment
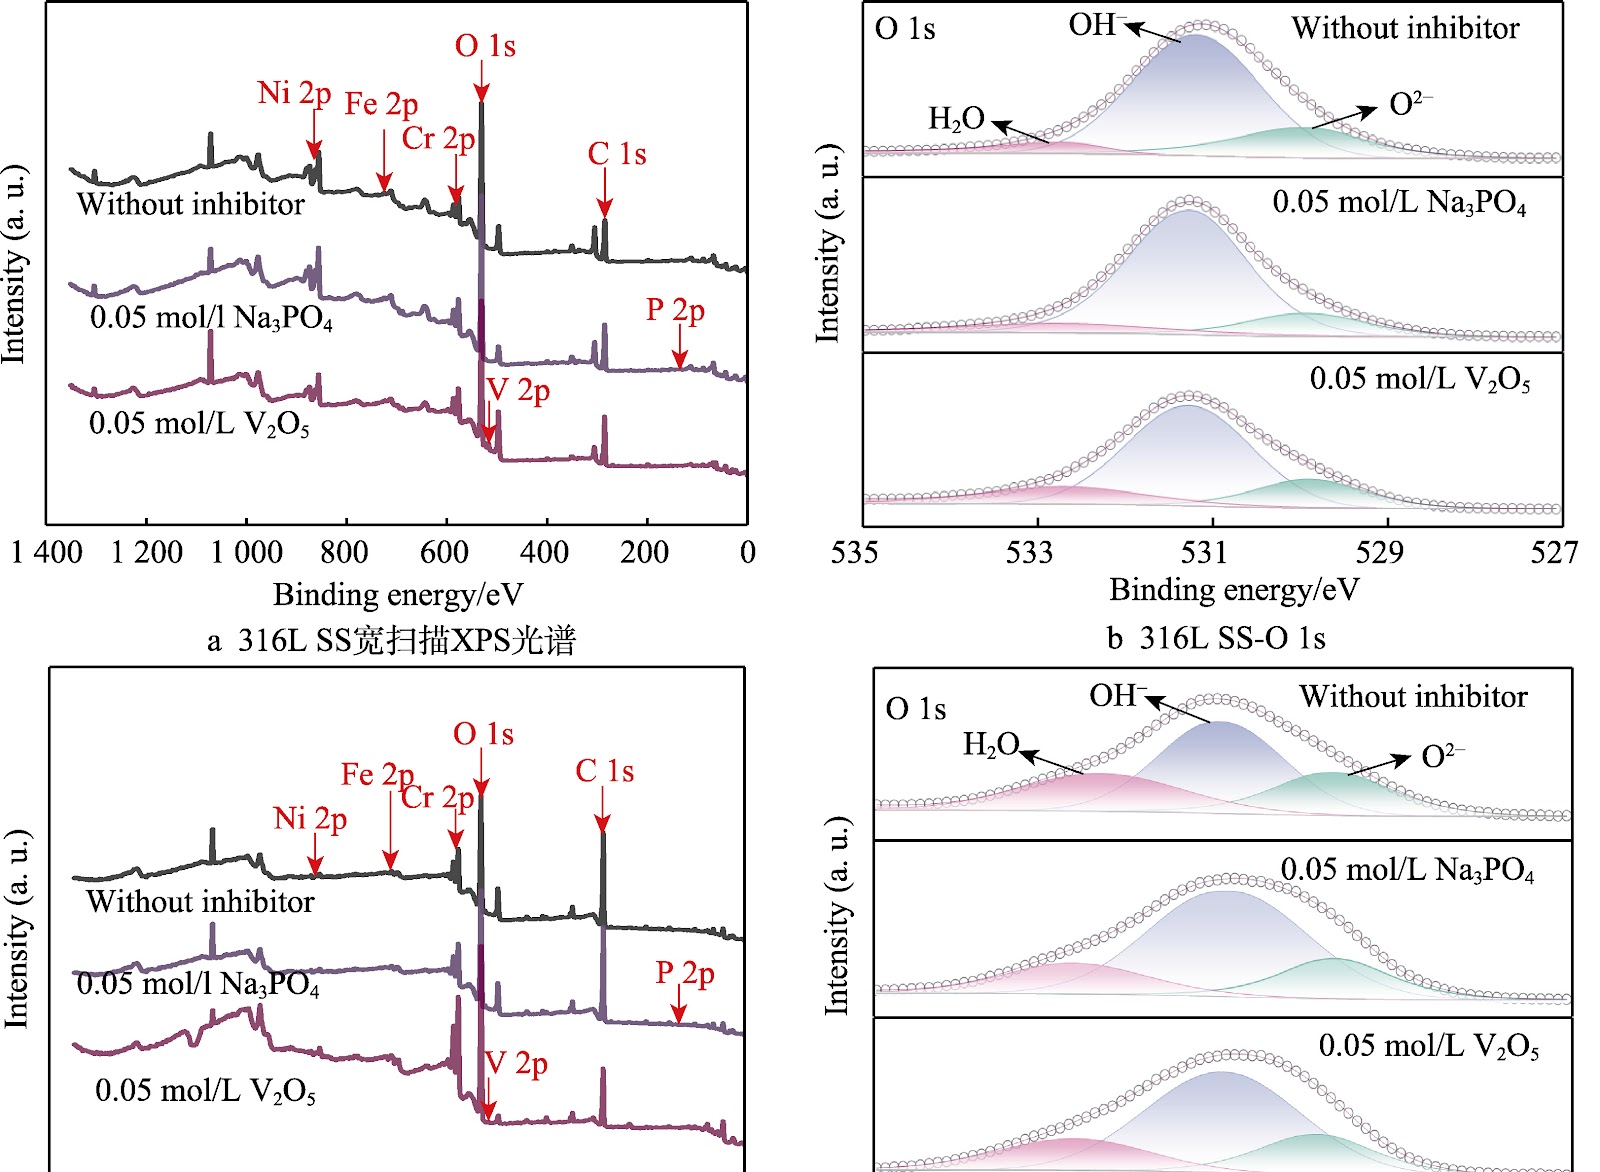
Alkaline seawater electrolysis for hydrogen production imposes severe corrosion on structural stainless steels, particularly in high-temperature, highly alkaline, chloride-rich electrolytes. This study evaluates four inorganic inhibitors—sodium molybdate (Na2MoO4), sodium tungstate (Na2WO4), sodium phosphate (Na3PO4), and vanadium pentoxide (V2O5)—for 316L austenitic stainless steel (316L SS) and 2205 duplex stainless steel (2205 DSS) in a simulated electrolytic seawater environment (6.0 mol/L NaOH, 2.0 mol/L NaCl, 90 °C). Potentiodynamic polarization, electrochemical impedance spectroscopy (EIS), and 14-day immersion tests quantified inhibition efficiency (IE). Surface morphology and film chemistry were characterized by SEM, optical profilometry (OP), and XPS. V2O5 exhibited the highest IE, reaching 79.90% for 316L SS and 89.58% for 2205 DSS at 0.05 mol/L, followed by Na3PO4 (83.33% for 2205 DSS). Na2MoO4 and Na2WO4 were least effective. EIS fitting revealed that V2O5 markedly increased film resistance (Rf) and charge-transfer resistance (Rct) (e.g., Rct = 29,770 Ω·cm², Rf = 923.50 Ω·cm² for 316L SS), indicating suppressed interfacial charge transfer. XPS confirmed the incorporation of V4+/V5+ and PO4³− species into the surface film, forming a dense, barrier-type vanadium/phosphate composite layer that mitigates corrosion. These findings establish V2O5 and Na3PO4 as promising inhibitors for stainless steel in harsh alkaline electrolytic seawater systems.
Influence of Temperature on Diffusion Behavior and Infiltration Layer Structure of Sherardizing on Structural Steel
Powder sherardizing on Q235 structural steel was conducted in a 70wt.% Zn–0.8wt.% NH4Cl–29.2wt.% α-Al2O3 activated pack at 340–400 °C for 2–10 h to establish the temperature-dependent growth kinetics, phase evolution, and corrosion performance of Zn–Fe intermetallic layers. Cross-sectional SEM/EDS and XRD show that all layers consist of δ and Γ phases, with Γ concentrated near the substrate; excessive Γ at 340 °C initiates interfacial cracking. Layer thickness increases monotonically with temperature and time, rising from 10.80 μm at 340 °C to 43.90 μm at 400 °C after 6 h, and from 12.10 μm at 2 h to 81.60 μm at 10 h at 380 °C. The Zn/Fe ratio and δ-phase fraction increase with temperature, yielding denser layers and improved corrosion resistance; at 380–400 °C, corrosion current densities fall to 1.16×10⁻⁶–9.78×10⁻⁷ A/cm². The diffusion coefficient at 380 °C is 2.341×10⁻¹³ m²/s. Prolonged holding beyond 6 h produces through-thickness cracks. DSC and microstructural evidence support a three-stage growth mechanism: formation of active Zn atoms via ZnCl2 decomposition, bidirectional Zn/Fe interdiffusion along substrate defects, and continuous inward advancement of the Zn–Fe intermetallic front. The optimal processing window is 380 °C for 6 h, yielding a ~36.1 μm crack-free layer with 84.1% δ phase and superior corrosion resistance.
Research Progress and Problem Analysis on Corrosion Prediction of Supercritical CO2 Transport Pipelines
Pipeline transport is the core of large-scale CO2 delivery in CCUS projects, and supercritical pipeline transport is the most economical and feasible method. However, inherent multicomponent impurities and complex aqueous phase precipitation make corrosion control difficult and costly. This review assesses corrosion mechanisms and prediction technologies for supercritical CO2 transport pipelines, focusing on numerical analysis, supporting experiments, and field application within comprehensive mechanistic models. Current understanding has clarified the effects of individual impurities (H2O, H2S, O2, SO2, N2O, N2, H2, CH4) and operating parameters, but synergistic mechanisms of mixed gases remain unresolved, lacking systematic quantitative description. Existing prediction models are limited in applicability to corrosion conditions, morphological matching, and comprehensiveness of factors. Experimental methods suffer from insufficient reliability, particularly in precise metering and replenishment of corrosive media under low water content and multicomponent impurity synergy. Field application faces challenges in rational model use and accurate extraction of field data. Future directions include: deepening research on synergistic effects of impurity gases and quantifying them via theoretical analysis to establish mapping between impurity concentration and corrosion rate; accelerating development of aqueous phase precipitation and distribution models, multicomponent impurity water chemistry models, thermodynamic and kinetic models for multicomponent reactions, and competitive formation/growth models for multiple product films; strengthening experimental techniques for precise metering and replenishment under low water and multicomponent synergy; and improving field application by understanding model parameter physical meanings, applicability boundaries, and ensuring reasonable input parameters and accurate field data extraction.
Research on Wear Resistance and Wear Mechanism of NM500 Steel in a Wide Temperature Range
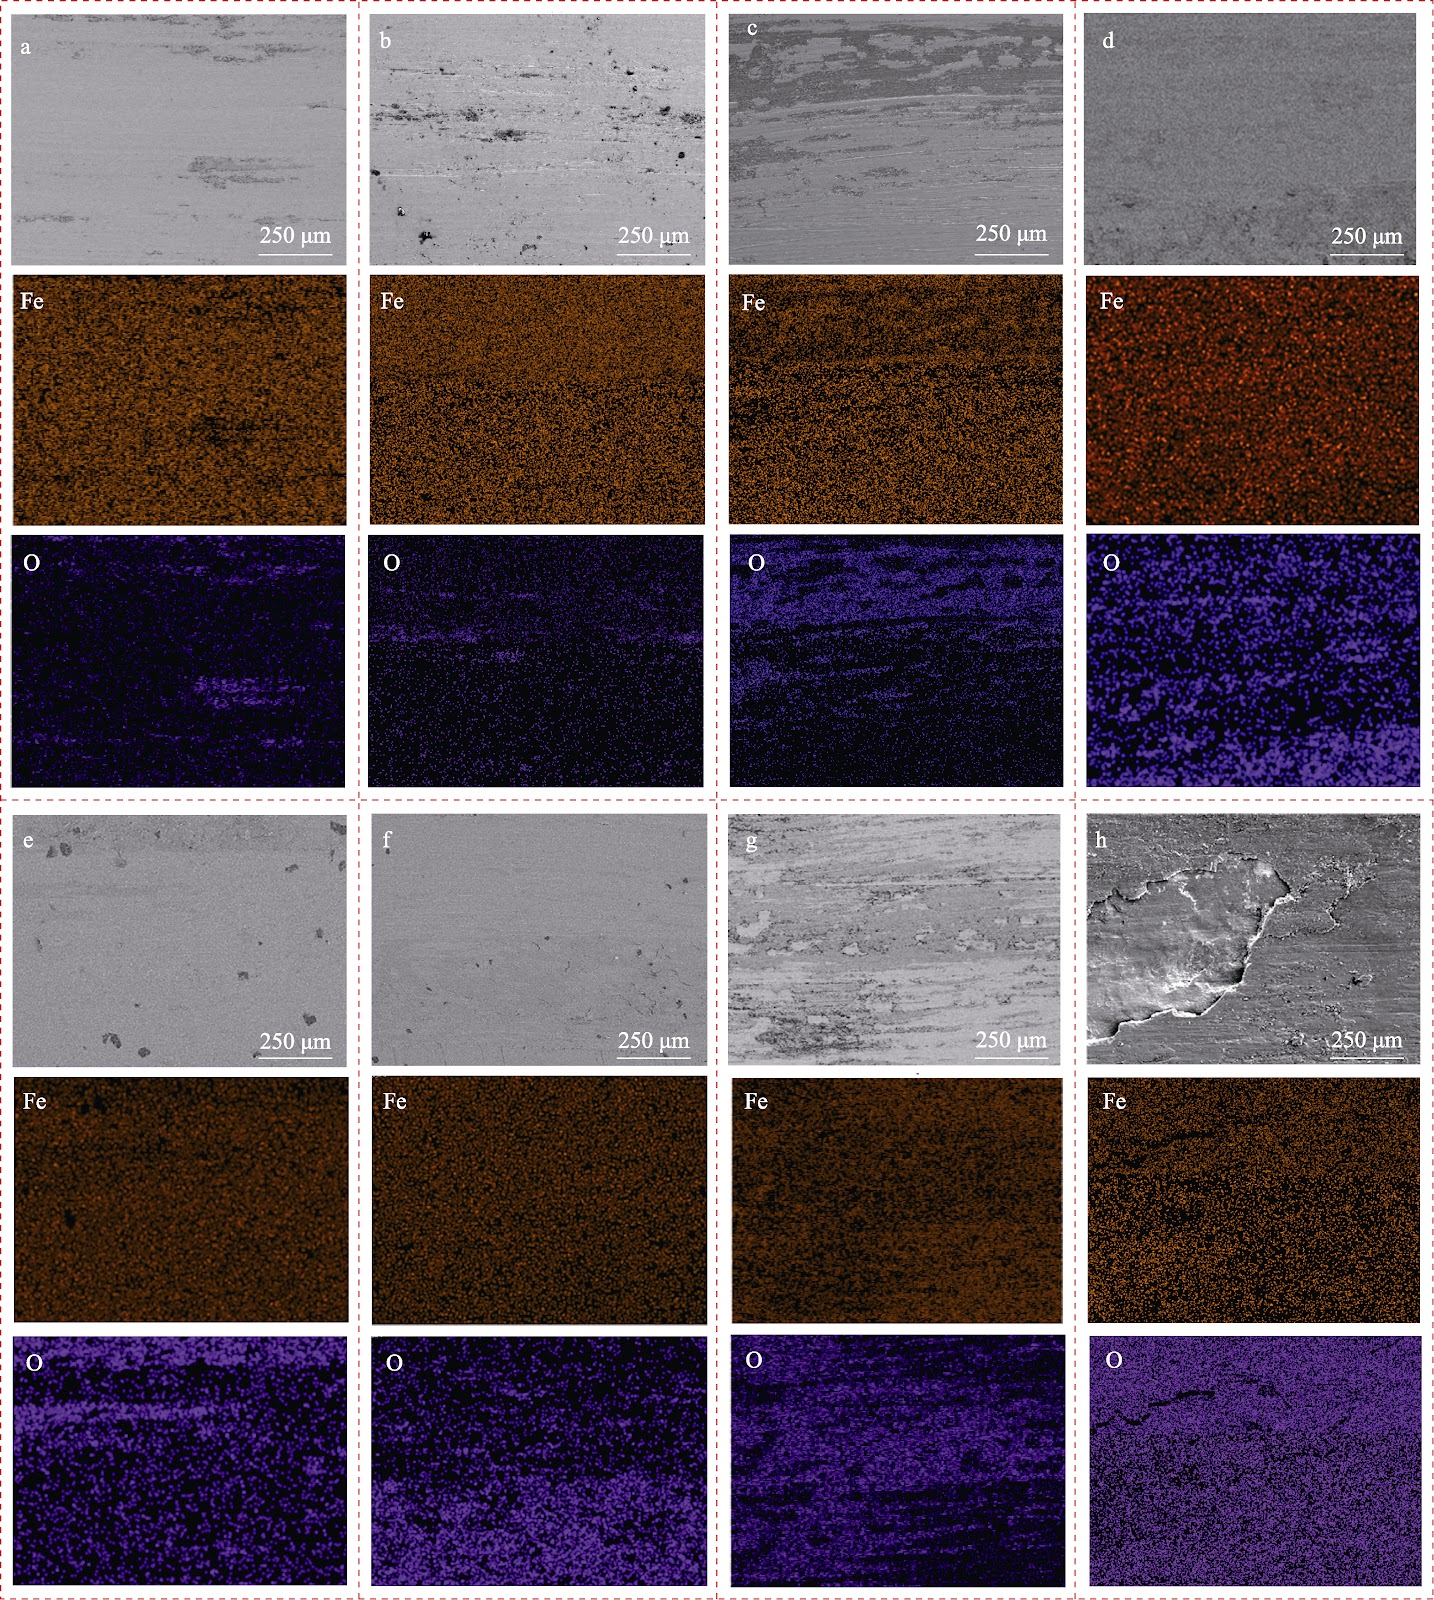
The tribological behavior of NM500 wear-resistant steel was systematically evaluated across a wide temperature range from −50 to 600 °C to elucidate the influence of temperature on wear resistance and to provide a theoretical basis for service life extension. Friction and wear tests were conducted using a high-temperature tribometer under a normal load of 150 N, rotational speed of 354 r/min, wear track diameter of 15 mm, and test duration of 60 minutes. The microstructure was characterized by SEM and EBSD, while worn surfaces were analyzed using XRD, SEM, and 3D laser confocal microscopy. NM500 steel exhibits a fine lath martensitic structure with a grain size of 7.08 μm, conferring high hardness and superior wear resistance. At cryogenic temperatures (−50, −25, 0 °C), the wear mechanism is predominantly abrasive wear, with a wear rate of only 1.29×10⁻⁶ mm3/(N·m). As temperature increases, oxide formation on the worn surface intensifies, friction coefficient decreases to a minimum of 0.3 (50% lower than at low temperature), and wear rate increases significantly: 18×10−6, 22.7×10⁻⁶, 46.7×10⁻⁶, and 128×10−6 mm3/(N·m) at 100, 200, 300, and 600 °C, respectively. The dominant wear mechanism transitions from abrasive wear at low temperatures to oxidative wear with adhesive wear at elevated temperatures. At 600 °C, thermal softening, reduced texture strength, and oxide film delamination exacerbate material loss, shifting the mechanism to oxidative wear as the primary mode with adhesive wear as secondary.