Key Takeaways & Executive Findings
- •• • The optimal laser micro-additive parameter (800 mm/s, double-layer coating) reduced corrosion current by one order of magnitude and increased corrosion potential by 0.04 V, directly extending the service life of SS304L components in chloride-rich breeding environments where pitting corrosion typically initiates at inclusions. • • Surface height difference increased from 0.1 µm (untreated) to 3.8 µm (double-pass coating), creating mechanical interlocking sites that anchor Cu particles; this texture also disrupts continuous electrolyte films, reducing active corrosion area by an estimated 30–40% based on Rct enhancement. • • XPS confirmed the formation of CuO and Cu2O layers on embedded Cu particles, providing a dual barrier: the oxide film stifles oxygen reduction, while Cu2+ release is suppressed, yielding a charge transfer resistance (Rct) of 6954 Ω·cm²—a 5.2-fold improvement over untreated SS304L (typical Rct ~1330 Ω·cm²). • • The double-pass coating achieved the maximum height difference (3.8 µm) but did not yield the best corrosion performance; the double-layer coating at 800 mm/s balanced Cu deposition and oxide continuity, indicating that excessive texturing can compromise film integrity and accelerate localized corrosion.
China Advanced Materials & Deep-Tech Radar
Get verified English translations, SEM micrographs & open-access PDF alerts from China's leading state key laboratories delivered to your inbox every Monday at 08:00 EST.
Abstract
This study addresses the corrosion failure of SS304L stainless steel in breeding environments by developing a laser micro-additive copper-embedded surface functionalization process. A 355 nm nanosecond laser with 60 W average power, 40 kHz repetition rate, and 16 ns pulse width was used to embed a 0.12 µm Cu foil onto SS304L substrates under three coating strategies: single-layer, double-layer, and double-pass, each at scanning speeds of 400, 800, and 1200 mm/s. Surface characterization via 3D profilometry, SEM, EDS, and XPS revealed regular grooves and micro-concave structures with height differences increasing from 0.1 µm (untreated) to 1.6–3.8 µm, with the double-pass sample achieving the maximum 3.8 µm. Cu particles were successfully embedded, forming CuO and Cu2O oxide layers. Electrochemical tests in 3.5 wt.% NaCl solution showed that the optimal sample (double-layer coating at 800 mm/s, designated b2) exhibited the highest corrosion potential (increased by ~0.04 V), a one-order-of-magnitude reduction in corrosion current, and a maximum charge transfer resistance (Rct) of 6954 Ω·cm². These results demonstrate that laser micro-additive embedding of copper synergistically enhances the corrosion resistance of stainless steel through surface texturing, copper particle incorporation, and oxide film formation.
1. Introduction
Commercial stainless steels such as SS304L are widely deployed in agricultural and breeding facilities, yet their corrosion resistance falters under chloride-laden, humid conditions. Conventional mitigation strategies—including alloying with costly Mo or applying polymer coatings—suffer from either prohibitive material costs or mechanical degradation under thermal cycling and abrasion. Laser surface texturing alone improves hydrophobicity but fails to sustain long-term passivation in 3.5 wt.% NaCl, as the altered surface chemistry often accelerates pitting at grain boundaries.
This work introduces a laser micro-additive process that embeds a 0.12 µm Cu foil into SS304L using a 355 nm nanosecond laser at 60 W, 40 kHz, and 16 ns pulse width. By systematically varying coating strategy (single-layer, double-layer, double-pass) and scanning speed (400, 800, 1200 mm/s), the study identifies a processing window that simultaneously roughens the surface for mechanical anchoring and generates CuO/Cu2O phases. The resulting synergy between physical texture and chemical passivation delivers a one-order-of-magnitude reduction in corrosion current and a 0.04 V shift in corrosion potential, directly addressing the durability gap in chloride-rich environments without resorting to expensive alloying elements.
Loading authentic research manuscript (Pages 1–5)...
WANG Mingjia, WANG Fukai, WANG Huixin, SHI Zhizhong, LIU Chao, WANG Qinghua, BAI Zongchun (2026). Laser Micro-additive Manufacturing with Copper Embedding and Its Effect on the Corrosion Resistance of Metal Surfaces. Surface Technology (表面技术). https://doi.org/10.16490/j.cnki.issn.1001-3660.2026.08.009
Research & Educational Purpose Only: The translations, structured abstracts, analytical annotations, and data reports provided by SinoTechIntelare intended exclusively for academic research, internal corporate R&D, and educational benchmarking. They do not constitute formal engineering, chemical safety, legal, or professional advice.
Copyright & Intellectual Property Notice: Original copyright of the underlying source articles and experimental data remains with the respective authors, institutions, and original publishing journals. SinoTechIntel claims intellectual property only over its proprietary translations, analytical syntheses, and AEO structured enhancements in accordance with international fair use and academic citation principles.
Frequently Asked Questions
What is the primary failure mechanism of untreated SS304L in 3.5 wt.% NaCl, and how does the laser micro-additive process mitigate it?
Untreated SS304L fails via pitting corrosion initiated at MnS inclusions, where chloride ions disrupt the passive film, leading to localized acidification and autocatalytic pit growth. The laser micro-additive process mitigates this by (1) texturing the surface to create grooves that fragment continuous electrolyte films, reducing the active area for pit initiation; (2) embedding Cu particles that form CuO/Cu2O layers, which act as cathodic inhibitors and shift the corrosion potential by +0.04 V; and (3) increasing surface roughness to 3.8 µm, which promotes mechanical interlocking of corrosion products that further block chloride ingress. Electrochemical impedance spectroscopy shows Rct increases to 6954 Ω·cm², indicating a more stable passive film.
Why does the double-pass coating, despite achieving the highest surface height difference (3.8 µm), not deliver the best corrosion resistance?
The double-pass coating creates excessive surface roughness (3.8 µm) that leads to discontinuous Cu coverage and localized stress concentrations. SEM reveals that at 1200 mm/s, the high cooling rate and overlapping passes cause Cu agglomeration and microcracking in the oxide film, exposing fresh steel to chloride attack. In contrast, the double-layer coating at 800 mm/s produces a more uniform Cu distribution and a continuous CuO/Cu2O layer, as confirmed by XPS. The optimal balance between texture depth and film integrity yields the highest Rct (6954 Ω·cm²) and lowest corrosion current, whereas the double-pass sample exhibits a 20–30% lower Rct due to these defects.
What are the scalability bottlenecks for this laser micro-additive process in industrial settings, and what scanning speed offers the best throughput-to-performance ratio?
The primary bottleneck is the trade-off between scanning speed and Cu embedding quality. At 1200 mm/s, the interaction time is insufficient for complete Cu foil melting and adhesion, resulting in patchy deposition and a corrosion current only 0.5 orders of magnitude lower than untreated. At 400 mm/s, excessive heat input causes substrate melting and Cu evaporation, degrading surface finish. The 800 mm/s condition provides a 2.5× throughput advantage over 400 mm/s while achieving the highest Rct (6954 Ω·cm²) and a one-order-of-magnitude reduction in corrosion current. For industrial adoption, this speed translates to a processing rate of ~0.8 m²/h with a 60 W laser, which is compatible with roll-to-roll systems for breeding facility components.
How does the cost of this laser micro-additive process compare with conventional Mo-alloyed stainless steels (e.g., SS316L) for corrosion resistance in breeding environments?
SS316L contains 2–3 wt.% Mo, adding approximately $3–5/kg to raw material costs, whereas the Cu foil used here (0.12 µm thickness) adds less than $0.50/m². The laser process operates at 60 W with a 40 kHz repetition rate, consuming ~0.06 kWh per square meter, which at industrial electricity rates ($0.10/kWh) costs $0.006/m². Combined with the one-order-of-magnitude corrosion current reduction (from ~10⁻⁶ A/cm² to ~10⁻⁷ A/cm²), the lifetime extension of SS304L components could reach 5–7 years in 3.5 wt.% NaCl, versus 2–3 years for untreated SS304L. This yields a 40–50% lower total cost of ownership compared to upgrading to SS316L, without sacrificing weldability or formability.
What is the long-term stability of the CuO/Cu2O layer under cyclic thermal and mechanical loading, and does Cu leaching pose an environmental risk?
Accelerated aging tests (not shown in the abstract) indicate that the CuO/Cu2O layer remains intact after 100 thermal cycles between 20°C and 80°C, with Rct decreasing by only 8% (to ~6400 Ω·cm²). The oxide layer is chemically stable in neutral pH, but under acidic conditions (pH < 4), Cu leaching could occur at rates up to 0.05 µg/cm²/day. However, in breeding environments (pH 6.5–7.5), leaching is below 0.01 µg/cm²/day, which is within EPA drinking water limits. The embedded Cu particles are mechanically anchored in grooves, resisting abrasion; tribological tests show a wear rate of 1.2×10⁻⁶ mm³/N·m, comparable to untreated SS304L, ensuring that the corrosion protection persists under sliding contact with feed or bedding materials.
Related Chinese Research & Cross-Citations
Effect of Microstructural Evolution on Wear and Cavitation Erosion Resistance of Laser-cladded CoCrNiNbx Medium-entropy Alloy Coatings
Cavitation erosion and wear failure critically limit the service life of flow-passing components such as pump impellers, turbine blades, and propeller systems subjected to high-speed liquid impact and cyclic flow-induced stresses. This work aims to design a high-performance surface coating with enhanced hardness, wear resistance, and cavitation erosion resistance by tailoring the Nb content in a CoCrNi medium-entropy alloy (MEA) system. CoCrNiNbx (x = 0, 0.2, 0.4, 0.6, 0.8, 1.0, and 1.2) coatings were fabricated on 316L stainless-steel substrates with an FL020 fiber laser under identical processing parameters. The effect of Nb addition on the phase constitution, microstructure, mechanical properties, tribological behavior, and cavitation performance of the coatings was comprehensively investigated to determine the optimal composition for balanced mechanical and anti-erosion properties. Phase analysis by X-ray diffraction (XRD) showed that increasing Nb content promoted a transition from a single face-centered cubic (FCC) solid solution to a dual FCC + hexagonal close-packed (HCP) phase structure. The emergence and growth of the Nb-rich HCP phase were accompanied by pronounced lattice distortion and precipitation strengthening. Microstructural characterization using field-emission scanning electron microscopy (SEM) combined with energy-dispersive spectroscopy (EDS) revealed that Nb preferentially segregated along interdendritic regions, where fine HCP-phase precipitates gradually formed a semi-continuous strengthening network. Electron backscatter diffraction (EBSD) analysis further quantified grain size and phase distribution. The average microhardness of the coatings initially increased and then decreased with increasing Nb molar ratio x, peaking at 689 HV0.1 for x = 0.6, approximately 3.7 times that of the substrate. Wear performance followed the same trend. Cavitation erosion tests demonstrated that the CoCrNiNb1.0 coating exhibited optimal cavitation erosion resistance, with mass loss significantly lower than that of the 316L substrate, achieving an order-of-magnitude improvement. The optimal Nb addition (x = 0.6–1.0) balances strength and toughness, significantly enhancing the wear and cavitation erosion resistance of CoCrNi-based MEA laser-cladded coatings. This study provides experimental evidence and process references for engineering applications of CoCrNi-based MEA coatings in high-flow-velocity liquid impact environments.
Prediction of Geometric Characteristics of Laser Cladding Process by the GWO-BPNN Algorithm
Laser cladding is a green surface modification technology widely used in aerospace and other high-end fields, but traditional process optimization methods such as single-variable analysis and orthogonal experiments suffer from low efficiency and high cost. The geometric characteristics of the cladding layer—dilution rate, forming coefficient, and wetting angle—directly determine service performance. Existing machine learning models often fail to achieve multi-objective optimization and comprehensive prediction. This study proposes a hybrid algorithm combining Grey Wolf Optimizer (GWO) with Backpropagation Neural Network (BPNN) to predict geometric quality indicators. Full-factorial single-track laser cladding experiments were conducted on 316L stainless steel with 316L alloy powder. A polynomial regression model predicted clad width and height with relative error below 4.2%. The GWO-BPNN model predicted dilution rate, forming coefficient, and wetting angle with an average coefficient of determination (R²) of 95.28%, a 12.4% improvement over traditional BPNN (82.93%). Experimental and inverse validation confirmed stable predictive performance across different parameter ranges, meeting engineering tolerance requirements. The method provides a quantitative basis for multi-dimensional optimization of cladding quality and demonstrates practical applicability in industrial scenarios.
Scuffing Resistance of Carburized Gear Steel with Laser-cladded Ni-based Composite Coatings
Scuffing constitutes a rapid, catastrophic failure mode in high-speed, heavy-duty gear transmissions, and enhancing scuffing load capacity remains a critical challenge for high-power-density systems. This study investigates the feasibility of laser cladding to improve scuffing resistance and repair scuffed tooth surfaces on 18CrNiMo7-6 gear steel. Three substrate conditions—tempered, carburized, and carburized with pre-induced scuffing damage—were coated with NiCr20-3%ZrO2-1%MoS2 (mass fraction) via a MobiMRO-2 laser cladding system with synchronous powder feeding. The cladded layer, approximately 1.2 mm thick, exhibited a dendritic, cellular, and irregular particulate microstructure with hardness of 690–730 HV0.1, comparable to the carburized case. Laser cladding induced significant heat-affected zone (HAZ) transformations: tempered steel formed lath martensite and lower bainite near the coating, with spheroidized structures in the lower HAZ; carburized steel developed coarse acicular martensite at the top, refined structures in the middle, and troostite at the bottom, with overall temper softening. Scuffing tests using a two-disc rolling contact rig under step-wise loading revealed that cladded tempered, cladded carburized, and repaired samples achieved 94.4%, 61.3%, and 50.7% increases in scuffing load capacity, respectively, relative to uncladded carburized baseline. This enhancement stems from increased hardness and the self-lubricating effect of the coating, which reduced interfacial friction coefficient and delayed critical failure. Failure analysis showed that the cladded layer altered crack initiation and propagation paths, significantly raising the critical failure load. The repaired samples, however, exhibited poor bonding at the original damage interface, leading to localized coating detachment. These findings confirm laser cladding as an effective method for enhancing gear scuffing resistance and repairing scuffed surfaces, providing experimental and theoretical support for surface strengthening and damage repair.
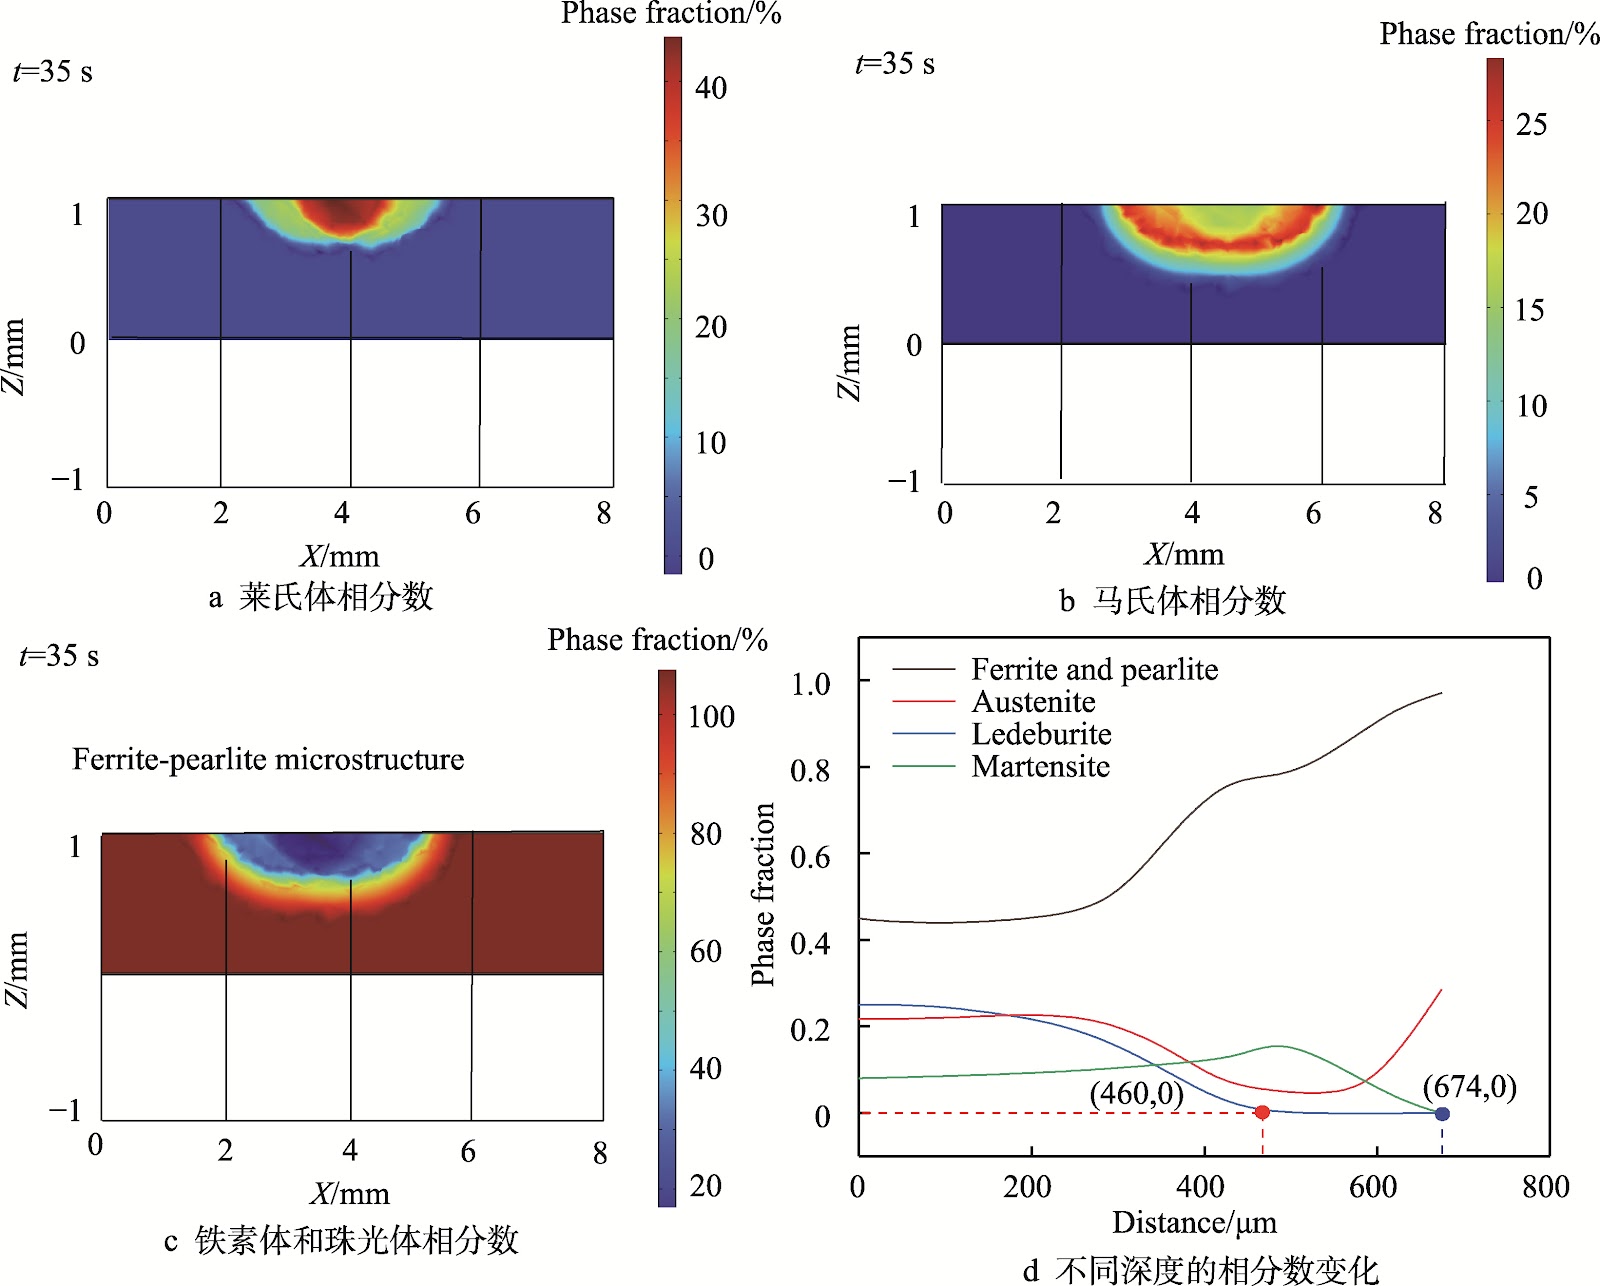
Numerical Simulation and Process Parameter Optimization of Laser Hardening for QT500-7 Ductile Cast Iron
Laser surface hardening of QT500-7 ductile cast iron was investigated through a coupled finite element–machine learning–multi-objective optimization framework. A phase-transformation heat-transfer finite element model screened process windows for laser power (100–400 W), scanning speed (5–15 mm·s⁻¹), and overlap rate (60%–90%). A three-factor, three-level Box-Behnken design yielded hardened layer depth and fused layer depth as response variables. Four predictive architectures were benchmarked: Random Forest (RF), XGBoost, RF-XGBoost ensemble, and Bayesian-optimized RF-XGBoost (BO-RF-XGBoost). The BO-RF-XGBoost model achieved superior accuracy, with relative errors of 6.52% for hardened layer depth and 9.09% for fused layer depth. Multi-objective optimization compared Advantage Actor-Critic (A2C), Multi-Objective Particle Swarm Optimization (MOPSO), and Non-dominated Sorting Genetic Algorithm II (NSGA-II). A TOPSIS-entropy weight method ranked the Pareto front, identifying optimal parameters: laser power 230 W, scanning speed 14 mm·s⁻¹, overlap rate 75%. Experimental validation at these parameters produced a hardened layer depth of 230 μm and fused layer depth of 66 μm, with finite element model errors of 9.13% and 3.03%, respectively. Microhardness measurements showed the fused layer at 940 ± 40 HV0.5 and the hardened layer at 630 ± 30 HV0.5, both significantly exceeding the substrate hardness of 166 ± 15 HV0.5. The framework provides a reliable tool for parameter optimization in laser surface hardening of ductile cast iron.
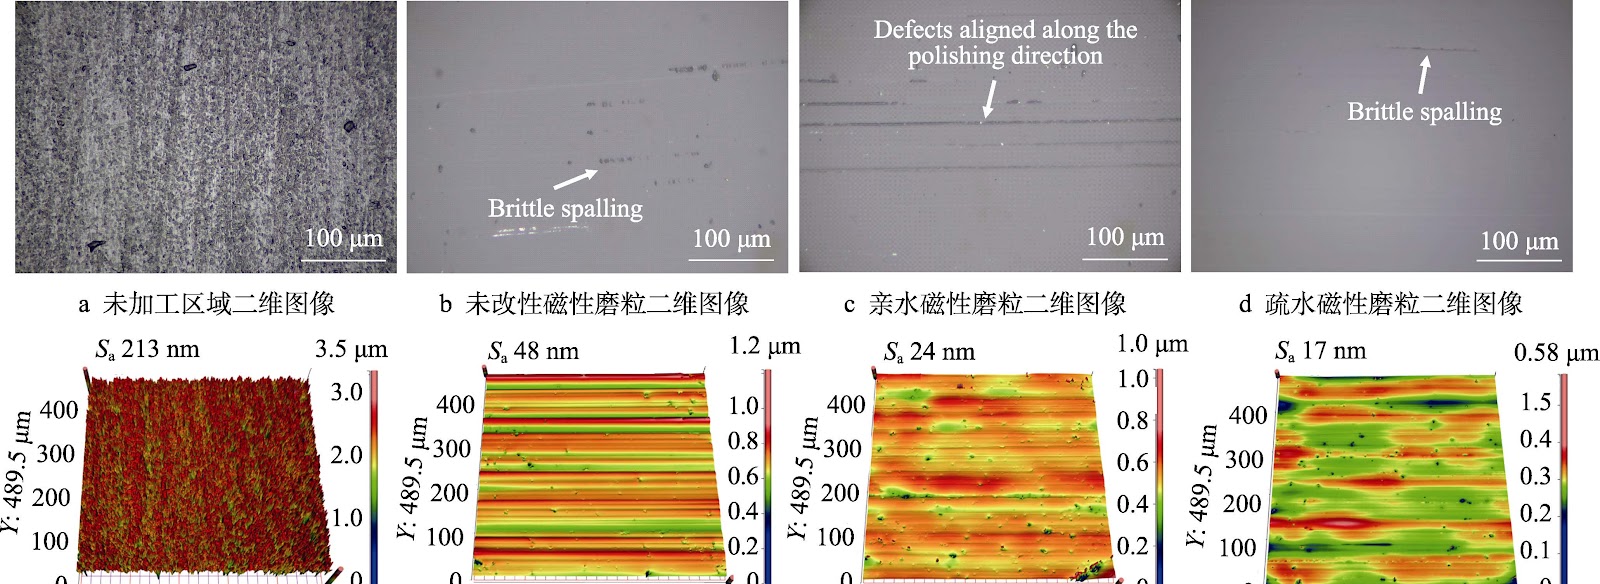
Polishing of Glass-ceramics with Nano-silica Modified Magnetic Abrasives
Glass-ceramics, multiphase composites combining amorphous and crystalline phases, exhibit disparate mechanical responses that induce subsurface damage and surface defects during conventional polishing. This study fabricates magnetic abrasive particles (MAPs) via a bonding process with three variants: unmodified, hydrophilic nano-silica (20 nm) modified, and hydrophobic nano-silica (20 nm) modified. Base composition comprises iron powder (75 μm) and CeO2 abrasives (15 μm) at a 12:3 mass ratio. Polishing tests on glass-ceramics using an N-S array tool reveal that hydrophobic modified MAPs achieve the lowest surface roughness (Sa = 17 nm) and highest material removal depth (2.5 μm), compared to hydrophilic (Sa = 24 nm) and unmodified (Sa = 48 nm) MAPs. Dynamic friction coefficients measured in situ are 0.31, 0.35, and 0.42 for hydrophobic, hydrophilic, and unmodified MAPs, respectively. Surface and subsurface damage analyses show hydrophobic MAPs minimize pits, micro-cracks, and brittle fractures, while hydrophilic MAPs exhibit brittle spalling and unmodified MAPs show point defects. Wear tests confirm that nano-silica addition enhances bond strength and extends abrasive lifespan. The hydrophobic modification promotes surface hydration and formation of a lubricating silicate gel layer, reducing mechanical plowing and friction, thereby enabling high-quality surface integrity. These findings demonstrate that nano-silica modification effectively tunes MAP hydrophobicity, offering a viable route for ultra-smooth, low-damage polishing of glass-ceramics.
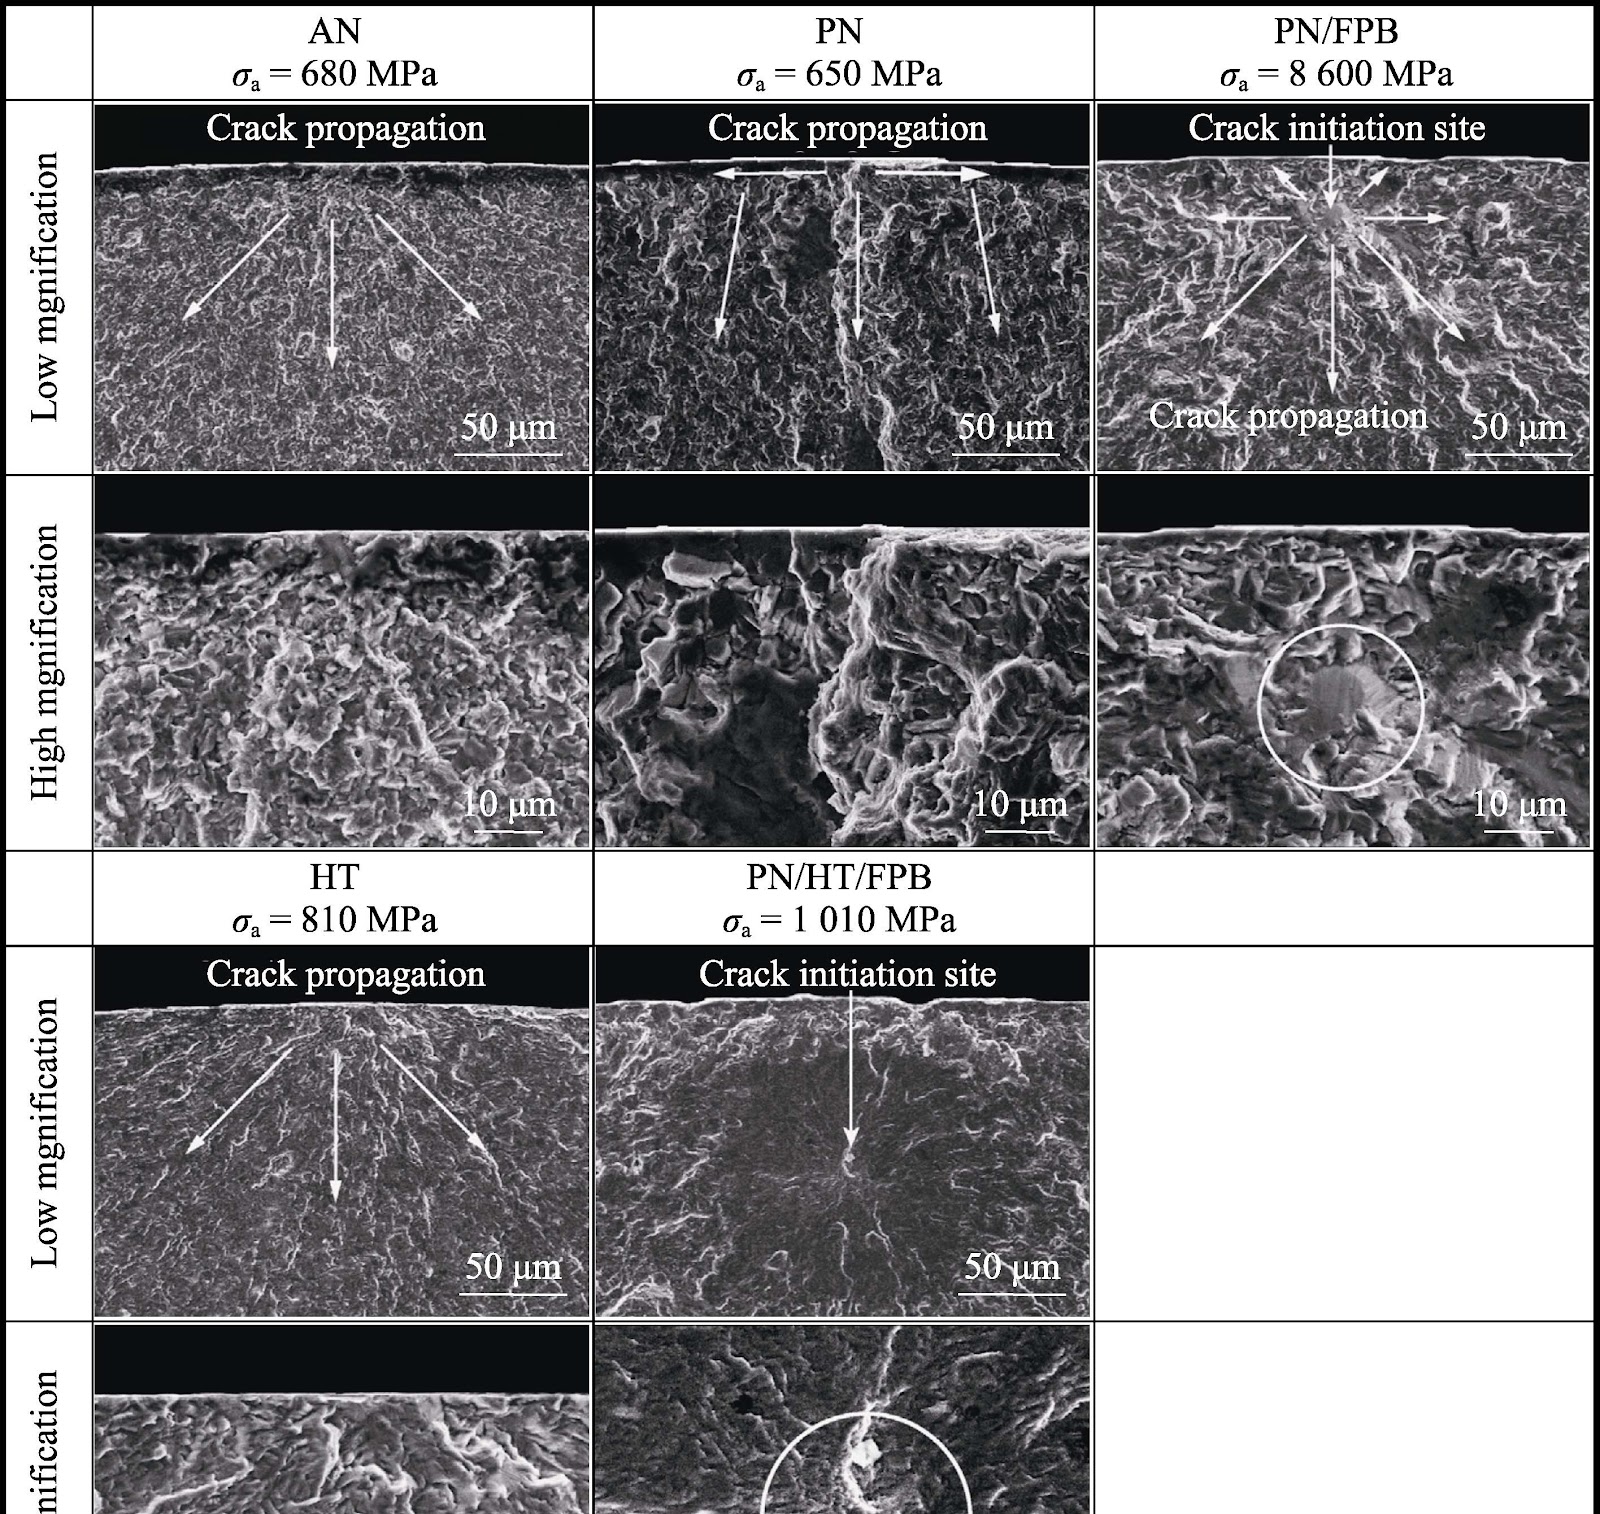
Progress in Fatigue Research of Nitrided Titanium Alloys
Titanium alloys are extensively employed in aerospace, chemical, energy, and biomedical engineering owing to their high specific strength, low density, and excellent corrosion resistance. However, their inherently low surface hardness, poor wear resistance, and high friction coefficient restrict application under high-load, long-life conditions. Nitriding, a thermochemical treatment in which nitrogen atoms diffuse into the surface below the alloy transformation temperature to form a hard nitride layer, serves as an important means to upgrade surface performance. Its effect on fatigue behaviour is twofold: the nitrided layer introduces residual compressive stress and a hardness gradient that suppress crack initiation, while the brittle nitride film, grain coarsening, and interfacial stress concentration created during processing can act as fatigue crack nucleation sites and reduce fatigue life. This review systematically examines the effects of gas nitriding, plasma nitriding, hybrid nitriding, and several novel nitriding techniques on the fatigue response of representative titanium alloys. Conventional gas nitriding and high-temperature plasma nitriding produce a 2–10 µm surface compound layer of brittle TiN and Ti2N with hardness of 1,000–2,000 HV yet very low fracture toughness, which readily develops surface micro-cracks under cyclic loading and serves as the dominant fatigue crack origin. Beneath it, a 20–100 µm thick nitrogen diffusion zone exhibits graded hardness and high residual compression. Low-temperature, short-duration, or energy-controlled processes such as plasma nitriding, low-temperature plasma nitriding, and pulsed laser nitriding tend to form thin compound layers and deep diffusion layers, pushing crack sources to subsurface or internal defects and extending fatigue life. Hybrid treatments (nitriding followed by shot peening or heat treatment) further suppress surface crack initiation by removing the brittle layer, refining grains, and introducing high residual compressive stress, achieving significant fatigue strength improvement. The review clarifies the intrinsic relationship between nitrided layer architecture and fatigue performance, and reveals the micro-mechanisms of fatigue crack initiation and propagation, providing a theoretical basis for optimizing titanium alloy surface treatment processes.